 English
 Português do Brasil
 Español
 简体中文

The drag tube conveyor It is a device used to transport bulk materials in various industrial segments. The Idugel Group specializes in mechanical or pneumatic transport solutions, and in this text, we will explain the advantages and application of tubular conveyors, comparing them with other types of transport.
What are tubular conveyors?
Tubular drag conveyors are equipment used to transport bulk materials, such as grains, cement, ores, chemicals and others. The transport is carried out in a closed tube, through a drag system, the system is composed of several parts, each one playing a fundamental role in the transport of materials. In the following, we will describe the main parts of the tubular conveyor:
- Tube: the tube is the main element of the tubular conveyor, being responsible for protecting the material during transport and ensuring the efficiency of the system. The tube can be made from different materials such as carbon steel, stainless steel or plastic and is designed to resist corrosion and wear.
- Drag chain or cable: The drag chain or cable is responsible for moving the material through the pipe. Chain is a more common option and can be used to haul heavy materials, while drag rope is more suitable for lighter materials.
- Drive: it is responsible for moving the chain or drag cable, which in turn moves the material through the tube. The actuation can be electric or pneumatic.
- Material inlet and outlet: The material inlets and outlets are the openings in the tube where material enters and exits the conveyor. These openings can be equipped with sealing systems to prevent the entry of air and to avoid the emission of dust.
- Cleaning devices: are responsible for removing the remaining material from the tube after transportation. This prevents contamination of other materials and ensures system efficiency. Specific cleaner solutions can be developed for each application, the Idugel Group specializes in this!
- Support system: it is responsible for keeping the conveyor in an upright position and protecting the pipe against vibrations and other impacts.
Advantages of transport by tubular conveyors
The tubular conveyor has several advantages over other types of bulk material transport. Some of these advantages include:
Reduction of dust emission
The transport of bulk materials is often associated with the emission of dust, which can be harmful to the health of employees and the environment. Tubular conveyors are efficient in reducing dust emission, as they transport the material in a closed tube, which prevents the material from being exposed to the air and spreading in the environment.
Low energy consumption
Tube conveyors feature low energy consumption compared to other types of bulk material transport. This is because tube conveyors operate with a low level of friction, which results in lower energy consumption.
Long distance transport
The tubular conveyor is ideal for transporting bulk materials over long distances. This is because transport is carried out continuously and reliably, which results in less downtime and less need for maintenance.
Transport of sensitive materials
Tubular conveyors are ideal for transporting sensitive materials such as chemicals, food and medicine. This is because the transport is carried out in a closed tube, which prevents contamination of the material by external agents, such as dust or humidity.
Comparison with other types of bulk material transport
The tubular conveyor has several advantages over other types of bulk material transport, such as pneumatic conveying, bucket elevator conveying and helical screw conveying.
pneumatic transport
Pneumatic conveying is a method of transporting bulk materials in which the material is conveyed in an air stream. While efficient in some situations, pneumatic conveying can be problematic in applications where conveyed material is sensitive to moisture or breakage. In addition, pneumatic conveying can generate high noise levels and can be more difficult to control compared to tube conveyor conveying.
Transport by bucket elevators
Bucket elevator conveying is a method of transporting bulk materials in which the material is conveyed vertically by means of buckets attached to a conveyor belt. While efficient for vertical transport, bucket elevator transport can be less efficient than tube conveyor transport, especially in terms of energy consumption and maintenance. Additionally, conveying via bucket elevators can be problematic in applications where the conveyed material is sensitive to breakage.
Transport by helical threads:
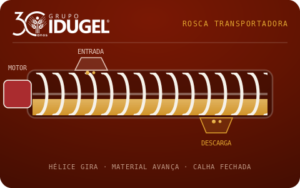
Screw Conveying is a bulk material conveying method in which the material is conveyed horizontally via a worm screw. While efficient in some situations, screw conveying can be problematic in applications where the conveyed material is sensitive to breakage or moisture. Furthermore, conveying via screw conveyors can be less efficient than conveying via tubular conveyors, especially in terms of energy consumption and maintenance.
Tube Conveyor Applications
Tube conveyors are widely used in various industrial segments, including food, chemical, pharmaceutical, mining and others. Some of the most common applications for tube conveyors include:
Transport of grains, cement, ores: The tubular conveyor is widely used in the transportation of grains such as wheat, corn, rice and soybeans. This is because tube conveyors are efficient in reducing dust emission and transporting over long distances.
Transport of sensitive products: Another use of tubular conveyors is in the transport of sensitive products, such as medicines, food, or materials that cannot suffer contamination or interference from the external environment, as well as damage resulting from high-speed transport.
Transport of chemicals and medicines: The tubular conveyor is ideal for the transport of chemical products and medicines, which require a safe and contamination-free transport. This equipment is capable of transporting these materials efficiently and safely, ensuring the quality of the transported products.
Transport and handling solutions from the Idugel Group: Transport beyond, with efficiency and precision!
Despite the benefits of each modality, it is important to choose a suitable transport concept for the specific needs of the process. The Idugel Group specializes in the design and manufacture of tubular, mechanical, pneumatic, mug or helical conveyors customized to meet the demands of each client. With an experienced team and state-of-the-art equipment, the Idugel Group is able to design efficient and reliable transport solutions for a wide variety of industries.
In addition, the Idugel Group offers complete technical support, from project design to system installation and maintenance. Customers can count on the company to provide custom solutions, replacement parts and maintenance services, ensuring their tube conveyor continues to run efficiently for years to come.
To resolve a material handling demand, count on a highly specialized team, contact us!